
Commercial Dishwasher Repair in Leander, TX
A dish machine that will not reach sanitising temperature is a health-code problem before it is a maintenance problem. We repair commercial warewashers — door-type, undercounter, conveyor and glasswashers, high-temp and chemical — for restaurants, bars and kitchens across Leander and the surrounding area. The $149 commercial diagnostic goes toward the repair, and you get a firm price before any part is replaced.
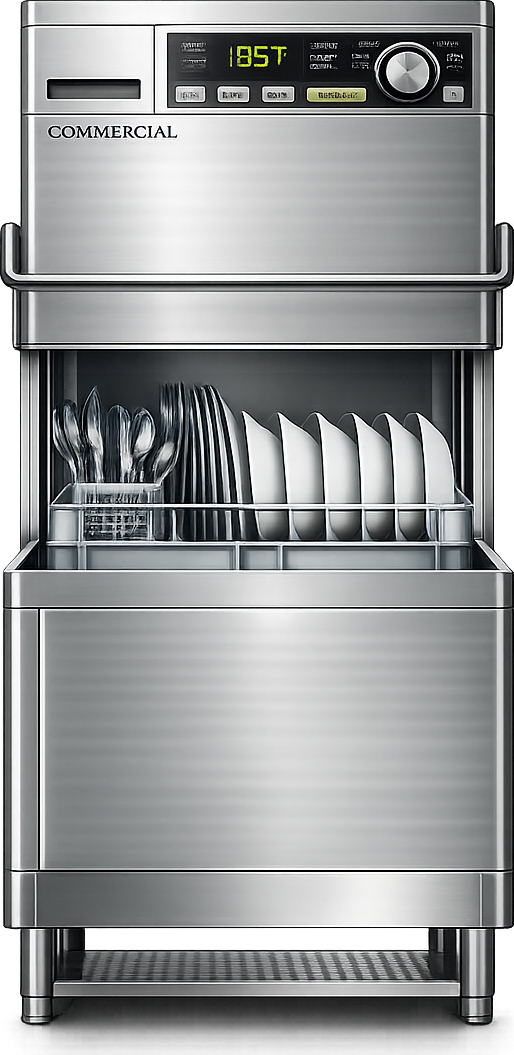
Common Commercial Dishwasher Problems in Leander
A commercial dish machine is measured, not judged by eye, and the numbers come from the manufacturers and from NSF. The figures below are what we check your machine against on site.
The final rinse is not reaching temperature
Common causes. A high-temperature machine sanitises with heat, and the standard is a final rinse of 180°F at the manifold over a wash tank running roughly 150 to 165°F depending on machine type. When the rinse falls short the causes are consistent: a booster heater off at the breaker or failed, incoming building water below what the booster was sized for, a booster element furred with scale, or rinse pressure out of range. The manufacturers publish the incoming minimums too — a built-in 30 kW booster expects around 110°F in, a 15 kW booster expects 140°F, and a high-temp machine with no booster needs 180°F arriving at the machine.
What we do. We read the machine’s own gauges through a full cycle and confirm them with an independent thermometer, then check the booster, the incoming water temperature and the rinse pressure. In Central Texas water the scaled booster element is the most common single finding, and deliming it restores the rinse without any part.
The machine runs but the dishes come out dirty
Common causes. Poor wash results are water, chemistry or mechanics. Blocked wash arm jets, a worn or missing end cap, scrap screens left out, a wash pump impeller worn, a tank running below its wash temperature, or a detergent feeder that has stopped dosing. Overloaded racks and dishes nested against each other produce exactly the same complaint with nothing wrong at all.
What we do. We pull and inspect the wash arms and jets, check the tank temperature against spec, and watch the detergent feeder actually dose. A machine with half its jets blocked by lime is a deliming job rather than a repair, and that distinction is worth knowing before anything is quoted.
Spots, film and cloudy glassware
Common causes. Spotting is hard water, rinse aid dosing, or a rinse that is too cool to flash off. Central Texas water leaves deposits on glass quickly, and a machine that was fine a year ago may simply be overdue for deliming. A rinse aid feeder that has run dry or lost its pickup tube causes it overnight.
What we do. We check rinse aid delivery, the final rinse temperature, and the state of the tank and arms. We will also say plainly if the real answer is water treatment rather than a repair, because on hard water that is often what it is.
The machine will not fill, or fills slowly
Common causes. A closed supply valve, a blocked inlet strainer, low building water pressure, or a failed fill solenoid or float. On machines that fill through the rinse line, a scaled rinse manifold slows the fill and lowers the rinse temperature at the same time.
What we do. We check the supply and the strainer first, then test the solenoid and the float. Strainers in this water block faster than most operators expect, and clearing one is a few minutes of work.
The machine will not drain, or the tank will not empty
Common causes. A blocked drain line, a scrap basket left full, a drain valve or its actuator stuck, or on pumped-drain machines a drain pump that has failed or jammed with debris. Standing water in the tank overnight also pushes the next day’s wash temperature down and the odour up.
What we do. We clear and test the drain path and operate the drain valve or pump directly to see whether it responds. A drain that works slowly rather than not at all is usually a partial blockage downstream of the machine.
The machine leaks
Common causes. Door gaskets and curtains on conveyor machines, the wash pump seal, tank fittings, or a drain connection. On conveyor machines missing or torn splash curtains throw water out of the tunnel and look like a leak from the machine itself.
What we do. We run the machine and find where the water actually escapes, then check curtains, gaskets and the pump seal. A pump seal leaking into the cabinet is a different repair from a worn gasket and they look identical on the floor.
A chemical-sanitising machine that is not sanitising
Common causes. Low-temperature machines sanitise with chemical in the final rinse at around 120°F rather than with heat, so the failure is nearly always the chemical side: an empty sanitiser container, a feed pump that has quit, a pickup tube out of the drum, or a squeeze tube worn through. Rinse pressure matters here too — too high and the sanitiser cannot be drawn into the rinse line properly.
What we do. We test the final rinse with a sanitiser test strip, then work back through the feeder, the tubing and the rinse pressure. Chemical feeders are usually supplied by the chemical company rather than the machine manufacturer, and we will tell you which side the fault is on.
Failing an inspection on the dish machine
Common causes. The usual failure is a final rinse that has drifted below 180°F while the kitchen kept running, because the machine does not stop you. On several platforms the low-rinse warning only posts a message and keeps the racks moving, and on some it ships switched off entirely. A booster that drifts over months fails an inspection on the first day somebody measures it.
What we do. We verify wash and rinse temperatures with an independent thermometer, document the readings, and correct what is causing the drift. We will also show you the daily check to run yourself, because a one-minute reading each shift is what keeps this from being a surprise.
Dish Machines We Service in Leander
We work on undercounter and glasswasher units, door-type and hood-type machines, single and multi-tank rack conveyors, and flight-type machines, both high-temperature with booster heaters and low-temperature chemical-sanitising.
Brands we service in Leander: Hobart, Jackson, CMA, Champion, Moyer Diebel, Insinger, Meiko, Fagor, Ecolab-supplied machines and Atosa.
What Commercial Dishwasher Repair Costs in Leander
Diagnostics are $149 for a commercial call, and that amount is credited toward the repair when you approve it. After the diagnosis you get a written estimate covering parts and labor, and nothing is replaced before you approve it. The final figure depends on what failed — a booster element, a thermostat or sensor, a fill solenoid, a wash or drain pump, a door gasket or a control — and whether the visit is a repair or a scheduled deliming.
Completed repairs carry a 3-month labor warranty from TakiDA LLC and a 1-year parts warranty against manufacturer defects.
Neighborhoods We Cover in Leander
We cover Leander as a whole and reach most commercial kitchens in the city within about twenty minutes, including the restaurants and bars along US-183 and around Old Town. Nearby Cedar Park, Georgetown, Liberty Hill and Round Rock are also in our service area.
Common Questions About Commercial Dishwasher Repair in Leander
What temperature does my dish machine actually have to hit?
On a high-temperature machine, roughly 150 to 165°F in the wash tank and 180°F at the final rinse manifold, which brings the dish surface to about 160°F. On a chemical-sanitising machine, around 120°F with the correct sanitiser concentration, verified with a test strip.
My machine shows the right temperature but we failed an inspection.
Built-in gauges drift, and they read at a different point from where an inspector measures. We confirm with an independent thermometer at the manifold and show you the difference, then fix whatever is causing it.
Does Leander water affect dish machines?
Heavily. Scale on the booster element and in the rinse manifold is the single most common cause of a drifting final rinse here. Deliming on a schedule prevents most of the calls on this page.
What does a commercial call cost?
The commercial diagnostic is $149, credited toward the repair when you approve the work. You get a written estimate before anything is replaced.
Book Commercial Dishwasher Service in Leander
Tell us the make and model, whether it is high-temp or chemical, and what it is doing — low rinse temperature, dirty results, spotting, a leak, or a message on the display. Tell us the gauge readings if the machine has them.
Reliable Commercial Dishwasher Repair in Leander, TX
-

Warewasher Faults We Handle
- Not reaching sanitizing temperature
- Dishes coming out dirty or filmed
- Will not fill or drain
- Booster heater not heating
- Wash or rinse arms not spraying
- Chemical not being drawn in
- Leaking at the door or drain
-
Warewashers We Service
- Undercounter dishwashers
- Door type and hood machines
- Conveyor and flight machines
- Glasswashers
- High temp and low temp units
- Hobart, Jackson, CMA, Champion
- Meiko, Moyer Diebel, Insinger
Commercial Dishwasher Brands We Repair
If your brand is not listed, contact us — we likely service it.
Why Homeowners & Businesses Choose TakiDA
-
 Quality WorkWe deliver professional appliance repair with attention to detail, proper diagnostics, and long-lasting results you can rely on.
-
 OEM / High-Quality PartsWe use OEM or high-quality replacement parts to ensure correct operation, reliability, and extended appliance lifespan.
-
 Same-Day / Next-Day ServiceFast response with same-day or next-day service to reduce downtime and get your appliances back in working order quickly.
-
 Clear PricingUpfront estimates with transparent pricing. No hidden fees, no surprises — you know the cost before work begins.
-
 EPA Certified & InsuredEPA Section 608 Universal certified and fully insured for residential and commercial repair, giving you peace of mind and protection.
-
 Warranty on Labor & PartsAll repairs are backed by a warranty on labor and installed parts for added confidence and long-term reliability.
